
Shandong Linru Import & Export Trading Co., Ltd. (operating seamlessly alongside key manufacturing divisions including Shandong Binzhou Feijin Import & Export Trading Co., Ltd.) stands as an elite professional enterprise integrating end-to-end industrial design, metallurgical fabrication, thermal engineering, and international distribution of commercial kitchen equipment.
With 15 years of continuous experience in the field, our enterprise has organically evolved from a specialized single-line manufacturer of high-output kitchen stoves into a globally recognized engineering powerhouse. Today, we manage a highly diversified portfolio of premium commercial food warmers, forced-convection holding cabinets, modular heat lamps, and industrial refrigeration equipment.
From the very beginning, we have been fiercely committed to refining our manufacturing methodologies step by step. We operate under the unwavering technical philosophy that long-term enterprise value is built exclusively upon zero-defect engineering, structural durability, and thermal efficiency. Only by maintaining rigorous quality controls can we earn and preserve the long-term trust of international OEMs, global restaurant franchises, and hotel procurement syndicates.

With 15 years of experience in commercial kitchen equipment manufacturing, Feijin / Shandong Linru is committed to continuous product refinement, rejecting low-cost, low-quality shortcuts to ensure every piece of equipment delivers long-term stability and operational peace of mind.
For refrigeration and heating products, Feijin Import & Export combines high manufacturing standards with deep OEM customization — guaranteeing full compliance with international standards while tailoring technical parameters to match exact client specifications.
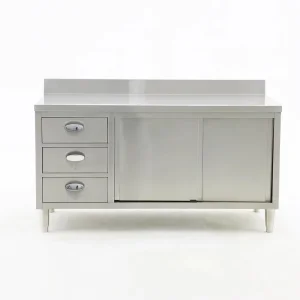
Our thermal and preparation equipment is built using high-grade AISI 304 or 201 stainless steel. We focus meticulously on internal structural framing, anti-corrosive seam welding, load-bearing integrity, and ergonomic finishing details to ensure maximum hygiene and longevity.
Global commercial food service operations face mounting pressure from escalating power tariffs and stringent carbon compliance standards (such as EU Ecodesign Directives and US ENERGY STAR standards). Modern custom food warmer units must incorporate high-density polyurethane (PU) insulated cavities, low-emissivity double-pane glass, and PTC (Positive Temperature Coefficient) heating elements to cut energy waste by up to 34% compared to legacy resistance-coil warmers.
Maintaining hot food consistently above the critical danger zone (60°C / 140°F) is non-negotiable for commercial operators to prevent pathogen growth (such as Clostridium perfringens). Modern OEM warmers feature multi-zone PID controllers that prevent heat decay across food pans, maintaining exact target temperatures within a tight tolerance of ±0.5°C.
Global QSR (Quick Service Restaurant) chains, ghost kitchens, and hotel buffets require tailor-made dimensional footprints, drop-in counter configurations, dual-temp holding zones, and branded fascia. Custom OEM engineering enables seamless integration into automated kitchen workflows and modular counter structures.
Our OEM Food Warmer Units are engineered from the ground up to solve the operational bottlenecks of mass catering and commercial holding. Below is an engineering overview of our proprietary equipment architecture:
| Engineering Component | Standard Specification | Custom OEM Option | Performance / Operational Benefit |
|---|---|---|---|
| Chassis & Exterior Shell | Food-grade AISI 201 / 304 Stainless Steel (0.8mm - 1.2mm thickness) | AISI 316 Acid-Resistant Steel / Custom Powder Coating / Titanium PVD Finish | Maximum structural rigidity, high resistance to food acids, and long operational life under heavy daily use. |
| Thermal Insulation Layer | High-density Cyclopentane Polyurethane Foam / Rockwool (50mm thickness) | Vacuum Insulation Panels (VIP) / Dual-Barrier Thermal Breaks | Prevents exterior shell overheating, reduces surface touch risk, and locks heat inside the holding cavity for minimal energy draw. |
| Heating Element Technology | Incoloy 840 Tubular Elements / Silicone Mat Heaters | Micro-thin Carbon Fiber Radiant Film / Precision Ceramic PTC Arrays | Ensures ultra-fast thermal response times, eliminates cold spots across food pans, and prevents burn-out risks. |
| Temperature Control Systems | Microprocessor PID Controller with LED Digital Display | Touchscreen HMI / IoT Telemetry / Modbus & Wi-Fi Remote Monitoring | Provides real-time temperature tracking, automated log retention for HACCP audits, and precise multi-zone control (±0.5°C). |
| Moisture Management | Passive Evaporative Water Pan with Anti-Spill Baffles | Active Ultrasonic Misting / Calibrated Steam Injection Systems | Prevents hot food from drying out, keeping fried items crisp and baked or stewed dishes moist over extended holding cycles. |
| Electrical Safety Ingress | IPX3 Moisture Splash Protection | IPX5 Washdown-Rated Sealed Electronics | Protects sensitive electronic components from water ingress during high-pressure commercial kitchen cleaning routines. |
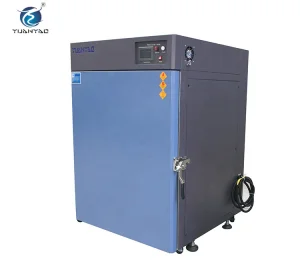
In addition to standard warming units, our facility produces specialized thermal processing vessels. As referenced in our core certifications, our heating equipment and commercial stoves hold full CCC (China Compulsory Certification) validation. Furthermore, our industrial jacketed kettles and pressurized thermal units are certified with both CCC and the prestigious National Pressure Vessel Manufacturing License, assuring institutional buyers of complete safety, mechanical integrity, and peace of mind under extreme operational pressures.
Designed for double-sided kitchen operations, allowing line cooks to insert freshly cooked items while front-of-house staff retrieve orders without thermal drop. Features angled gravity slides and micro-climate heating zone technology.
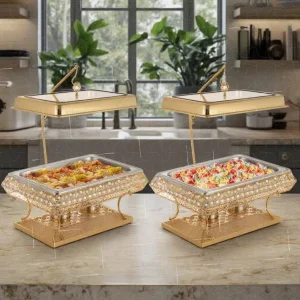
Sleek, under-counter integrated warmers featuring concealed induction heating coils, anti-reflective tempered glass sneeze guards, and custom brass or rose-gold decorative plating for upscale dining environments.
Combines overhead infrared heat lamps with bottom heated granite or stainless steel decks. Maintains fried chicken, rotisserie meats, and ready-to-eat meals at optimal serving temperatures with high visual appeal.
Mobile insulated holding cabinets built with perimeter bumpers, heavy-duty casters, and emergency thermal retention features designed to keep meals warm during long distribution routes across large facility campuses.
We are actively researching the integration of non-toxic phase-change materials into cabinet double walls. PCMs absorb heat energy during peak electrical cycles and passively radiate heat back into the warming chamber during power outages or transit, cutting energy draw by over 40%.
Next-gen OEM warmer controls integrate AI algorithms that learn kitchen peak usage patterns. By predicting heavy drawer usage times, the system pre-heats zones dynamically and scales back power during lulls, minimizing thermal stress and maximizing ingredient shelf life.
Through integrated Modbus and IoT communication protocols, enterprise food managers can track holding temperatures across hundreds of franchise locations simultaneously from a central dashboard, ensuring absolute HACCP audit compliance automatically.


 Linru Kitchen Equipment